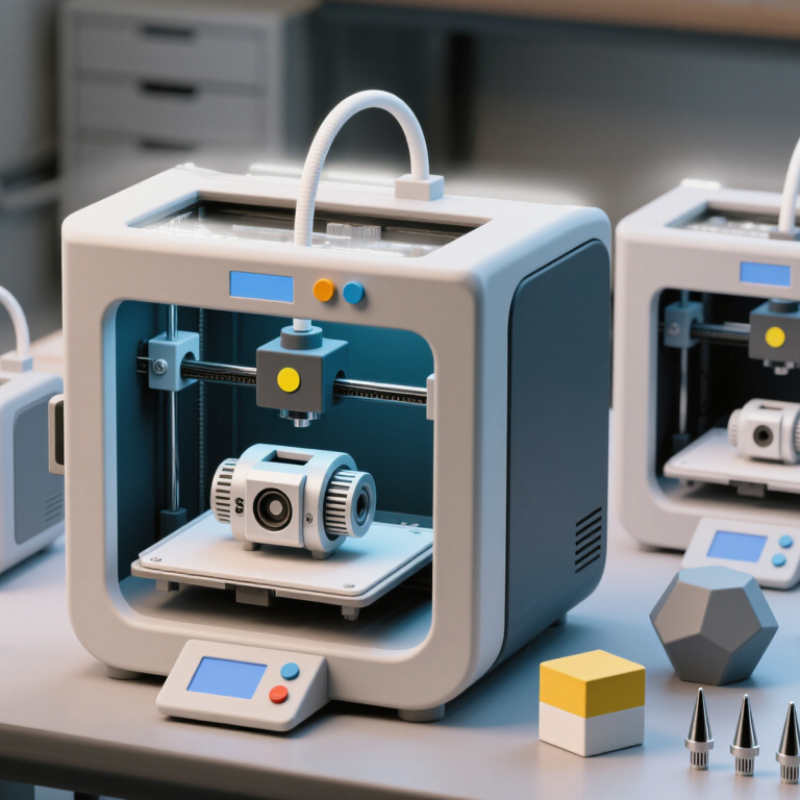
Choosing the best 3D Printer begins with understanding what you will actually make. A compact machine may suit miniatures, classroom projects, and replacement brackets. A larger model may handle prototypes, tool organizers, or functional household parts. Your decision should match your workspace, materials, skills, and patience.
Real experience often reveals details that product pages overlook. A quiet printer can still vibrate on a lightweight desk. A fast printer may require careful calibration and stronger ventilation. Check the build volume, nozzle temperature, heated bed, layer resolution, and compatible filament types. Also examine slicer software, spare parts, warranty support, and independent user reviews. These factors affect the printer long after the first successful test print.
Safety matters. Keep the machine on a stable, heat-resistant surface. Follow the manufacturer’s guidance for ventilation and electrical use. Avoid printing materials that your workspace cannot safely manage. Total cost matters, too. Filament, replacement nozzles, maintenance tools, and failed prints can change the budget quickly.
There is no universal winner.
A reliable recommendation must consider your real routine, not only impressive specifications. Beginners may value automatic bed leveling and simple software. Experienced users may prefer open settings and upgrade options. I have found that convenience sometimes limits control, while flexibility often increases maintenance. That trade-off deserves honest reflection. This guide will compare practical choices, common mistakes, and long-term value, helping you select a 3D Printer with greater confidence.
Classify the Job with ISO/ASTM 52900: FDM, Vat Photopolymerization, or PBF
How to Choose the Best 3D Printer for Your Needs?
Choosing a 3D printer becomes clearer when the job is classified by ISO/ASTM 52900. The standard groups processes by how they create each layer. In practical terms, ask what the part must survive, show, or reproduce. I begin with function, tolerances, surface finish, and production volume. Material availability and post-processing also matter. A beautiful sample can hide poor dimensional control.
FDM FDM, known in the standard as material extrusion, suits prototypes, fixtures, housings, and large functional parts. It usually offers simpler operation and lower material waste. Layer direction still affects strength. Keep that in mind.
Warping may appear around sharp corners, especially with temperature-sensitive materials. My first choice is not always right; a quick test piece can prevent a costly full-size failure.
Vat photopolymerization works well for small parts requiring fine details, smooth surfaces, or accurate visual models. However, printed parts may need washing, curing, and careful support removal. PBF, or powder bed fusion, is better for complex functional geometries and parts that benefit from internal channels. It reduces many support structures, but powder handling, thermal distortion, and post-processing demand trained operators. Measure real parts, not only screen models. The result can still surprise you.
FAQS
Use 0.10–0.30 mm layers for common FDM work.
SLA suits miniature text, jewelry-style forms, and complex decorative details. Typical layers range from 25 to 100 µm. At 25 µm, surfaces can look impressive. Cleaning and curing require extra care. Very extra care.
Measure the smallest feature you actually need to see. For 0.5 mm lettering, 100 µm layers may be enough. Functional parts often need strength and dimensional accuracy more than smooth surfaces. I once selected maximum detail and gained little visible improvement.
Measure your largest expected part by width, depth, and height. Add room for supports, brims, and positioning mistakes. A 220 × 220 × 250 mm space suits many household parts and prototypes. Larger parts may need splitting, sanding, and joining. That can weaken them.
Yes, a 0.4 mm nozzle balances detail, material flow, and print time. It works well for general-purpose printing. Nozzle size alone does not control detail. Cooling, extrusion settings, layer height, and movement also matter.
Run a small weekly test with a functional part. Record material use, total time, and final dimensions. Compare the result with your design. Advertised speed may not reflect real output. I still underestimate waiting time.
Count material, supports, failed starts, cleaning, curing, and protective equipment. Filament can appear cheap until wasted material accumulates. Resin may provide finer detail but requires more post-processing. Measure cost per successful finished component, not purchase price alone.
Use a plug-in energy meter during warm-up, printing, cooling, and idle periods. Record the finished part’s weight and total production time. Include ventilation and post-processing in the calculation. My early comparison counted only printer wattage. That was incomplete. Temperature, calibration, and software settings can change the results.
Conclusion
Choosing the best 3D Printer begins with identifying the type of work you need to complete. Using the ISO/ASTM 52900 framework, common processes include FDM for practical, durable parts, vat photopolymerization for fine detail and smooth surfaces, and powder bed fusion for complex, high-performance components. Define your required resolution early: FDM layers commonly range from 0.10 to 0.30 mm, while SLA-style systems may achieve layers of approximately 25–100 µm.
Next, evaluate build volume, nozzle size, printing speed, and expected production throughput. A standard 0.4 mm nozzle offers a useful balance between detail and efficiency, but larger or smaller options may better suit specific projects. Compare compatible materials, maintenance needs, energy consumption, and total operating costs using relevant ASTM F42 data. Finally, verify dimensional accuracy, repeatability, ventilation, electrical protection, and user safety through recognized NIST measurement methods and UL 2904 testing principles. This systematic approach helps match printer capabilities with realistic performance, budget, and workspace requirements.