High-Precision Machinery & Industrial Solutions
Featured Product Matrix & Custom Engineering
Explore our TÜV-verified industrial equipment lines, featuring heavy-duty structural metal frameworks, advanced CNC controls, electro-hydraulic servo synchronization, and rugged build compliance.
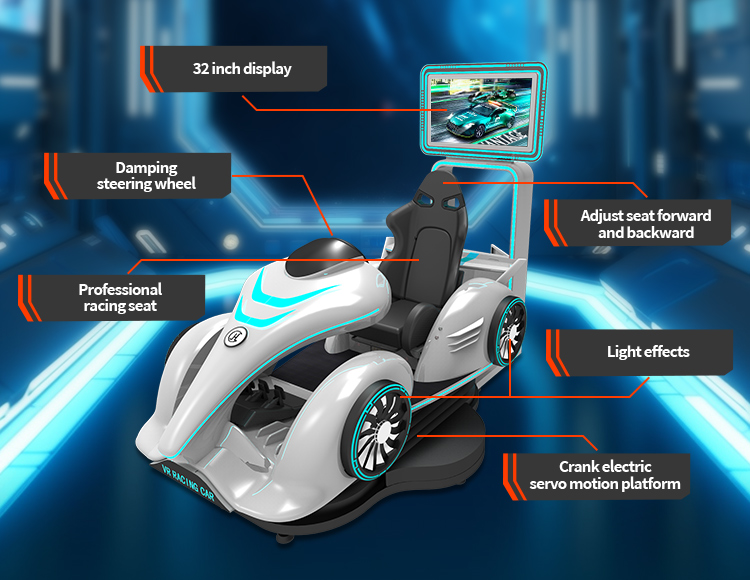
New 9D VR Driving Game Simulator Indoor Amusement Product Franchise Virtual Reality Vr Racing Karting Cart Games Metal Material
View Product Details
Children's Indoor AR Football Penalty Game Shootout Simulator Big Screen Projector with Metal Construction for Outdoors
View Product Details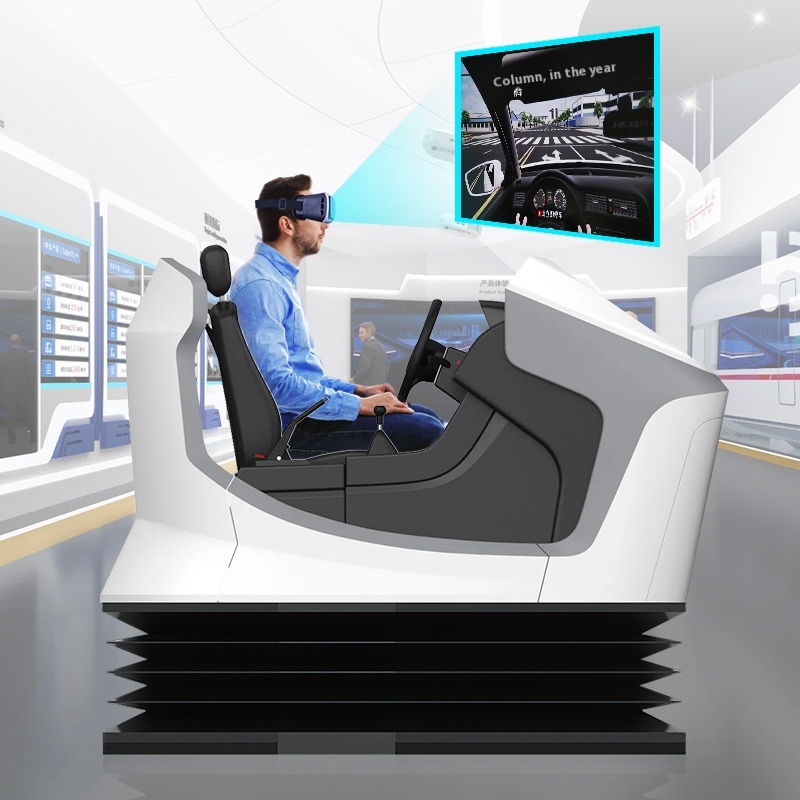
VR Car Driving Simulator Virtual Training System for Driving School & Home Shopping Mall Suitable Test Subject 2 & 3 Equipment
View Product Details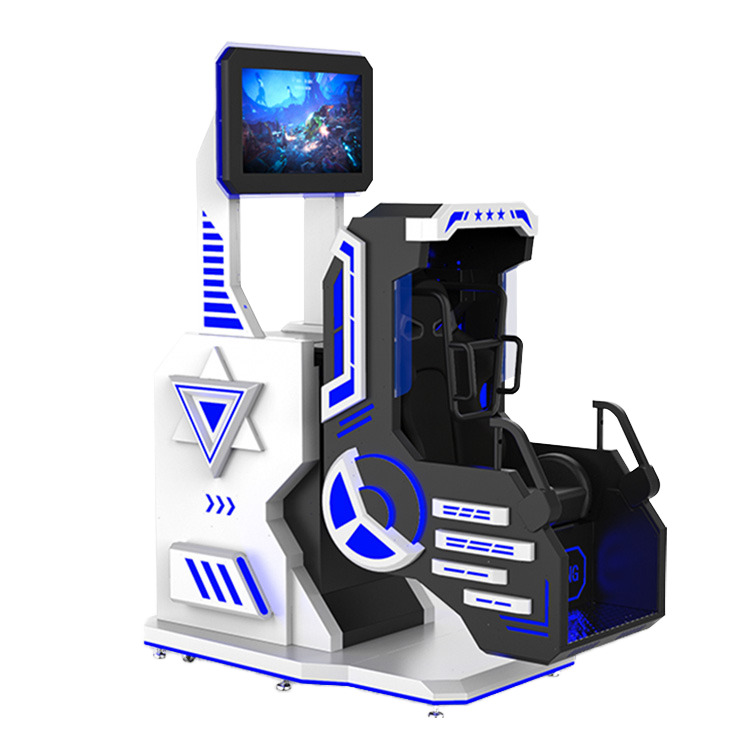
All-In-One VR Aircraft Equipment 360 Degree Rotating Seat Simulation Virtual Reality Flight Roller Coaster Big Shopping Mall
View Product Details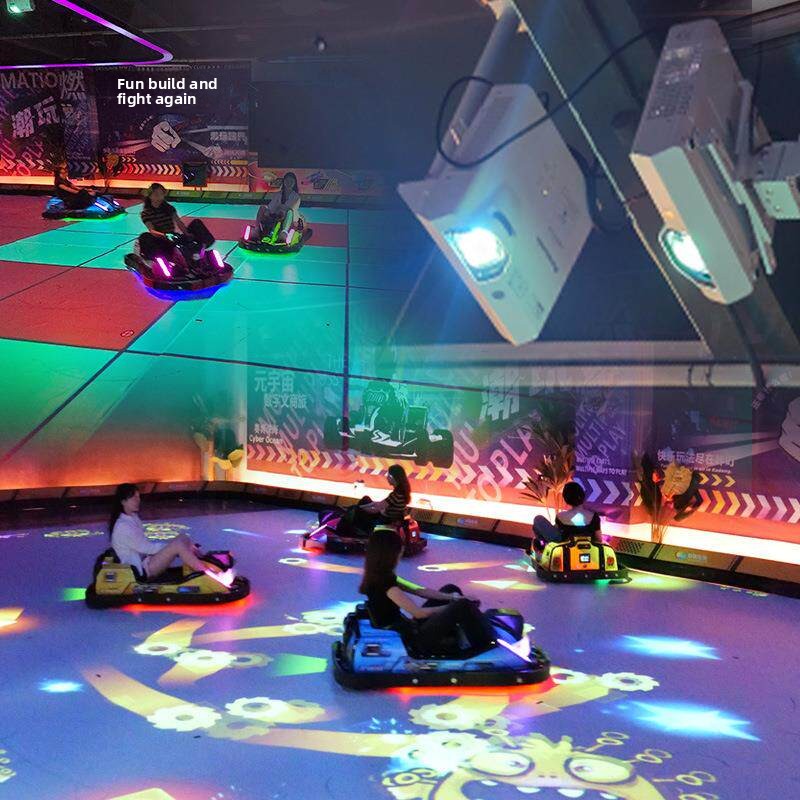
Longcheng Light and Shadow VR Kart Projection Interactive Snake Mario Immersive AR Holographic Migration Bumper Car
View Product Details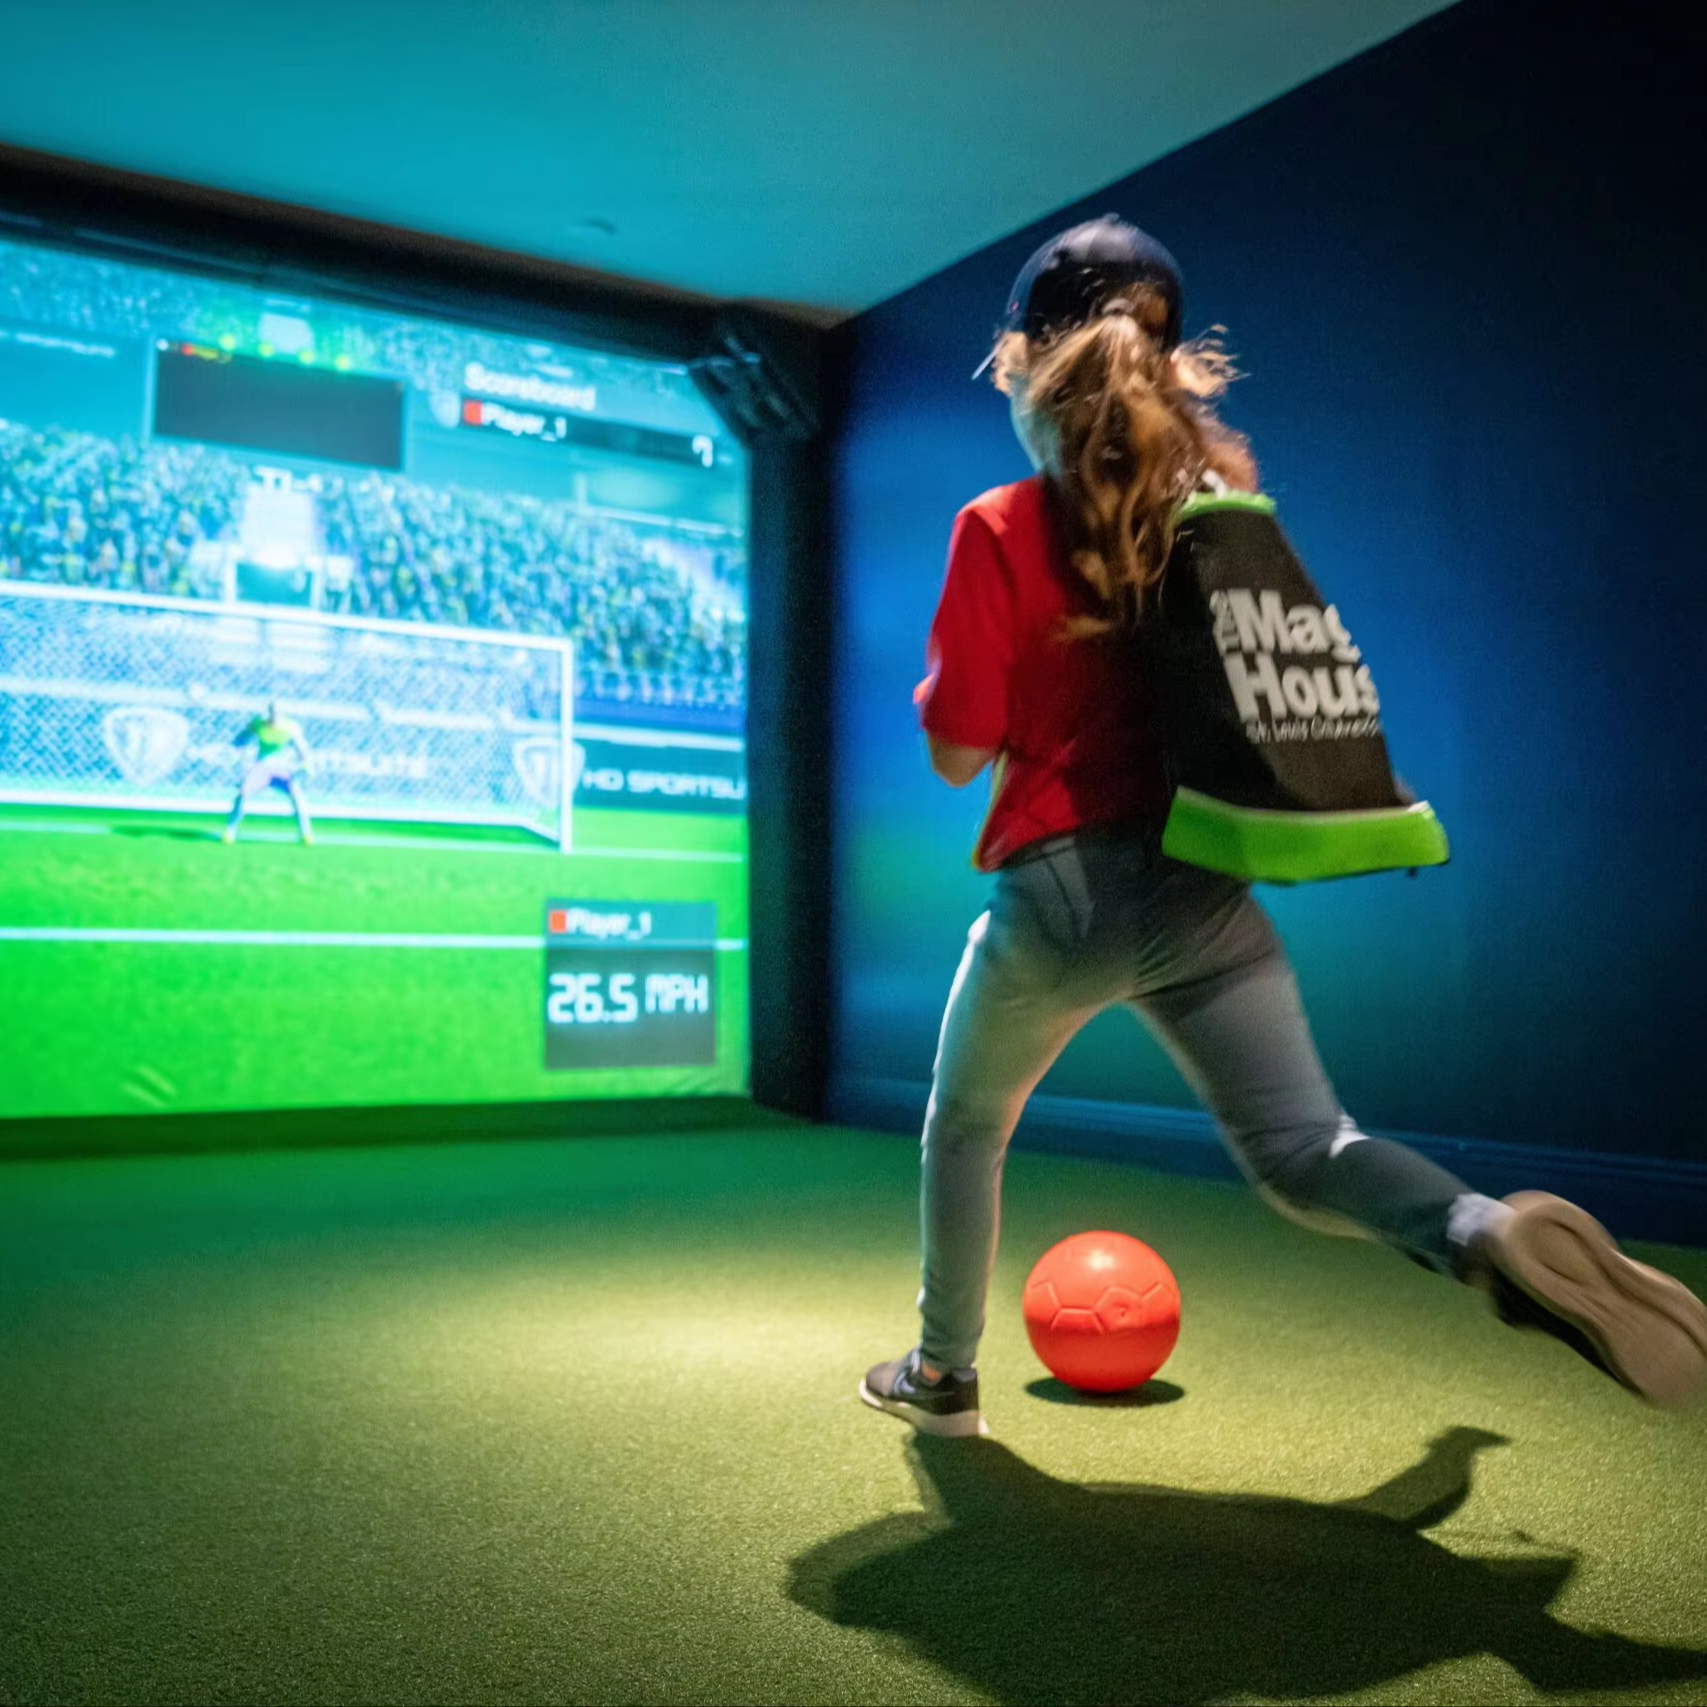
Indoor AR Football Simulator Projector for Home School Mall Entertainment Steel Educational Tool
View Product Details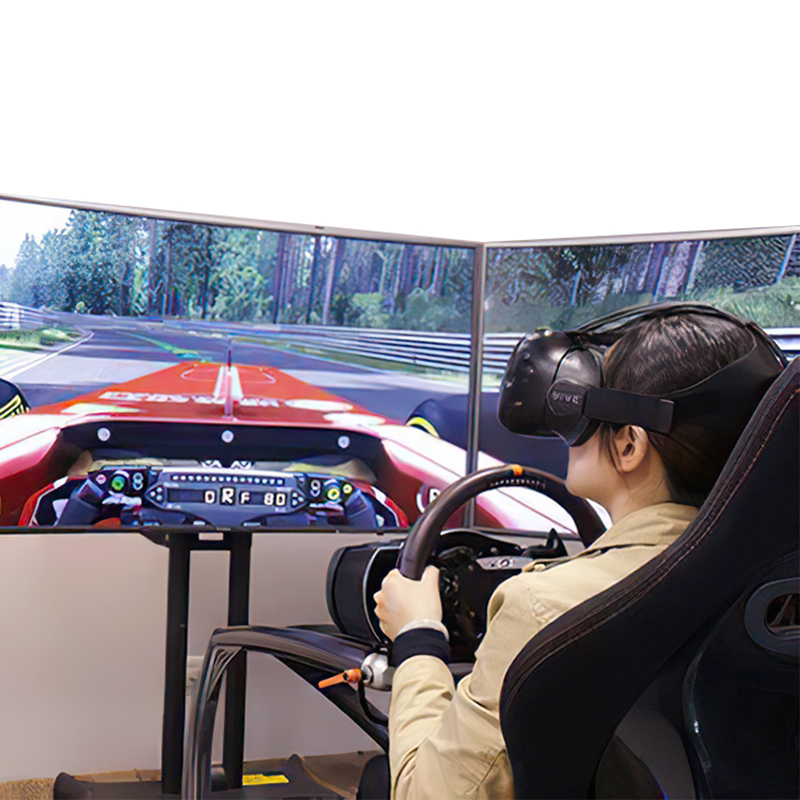
Full Set VR Racing Somatosensory Simulator Indoor PC Car Simulation with Traffic Experience Metal and Plastic Equipment
View Product Details
E-E-A-T Technical Framework
Engineering Compliance: CE Certified Bending Machine Standards
A comprehensive analysis of European Union safety directives, structural rigidity criteria, risk mitigation engineering, and compliance verification protocols for modern sheet metal processing equipment.
100%
CE Machinery Directive 2006/42/EC
±0.01mm
Ram Positioning Accuracy
EN 12622
Hydraulic Press Brake Safety Standard
2,000 m²
TÜV Rheinland Audited Facility
Navigating CE Marking Compliance for Press Brakes & Bending Machines
In the global metal fabrication industry, securing genuine CE Certification for industrial bending machinery is far more than a regulatory checkbox—it represents a fundamental engineering commitment to operational safety, structural integrity, and electromagnetic compatibility. Original Equipment Manufacturers (OEMs) and factory operators across Europe, North America, and high-growth industrial hubs must ensure that sheet metal forming equipment complies with the stringent requirements of the EU Machinery Directive 2006/42/EC, the Electromagnetic Compatibility Directive (EMC) 2014/30/EU, and the Low Voltage Directive (LVD) 2014/35/EU.
Specifically for hydraulic, electric, and hybrid CNC press brakes, compliance hinges upon adherence to EN 12622 (Machine tools — Safety — Hydraulic press brakes). This harmonized European standard establishes non-negotiable mandates regarding the safeguarding of the pinch-point zone where the upper punch contacts the bottom die. Modern certified manufacturers implement active optical protection devices (AOPDs) such as laser curtain safeguarding (e.g., Fiessler AKAS, DSP, or Lazer Safe systems) integrated directly into the safety PLC controller to enable high-speed closing movements while mitigating operator injury risk down to zero millimetres of overrun distance.
Information Gain Insight: Genuine CE compliance demands documented Risk Assessments under EN ISO 12100, mandatory dual-channel safety monitoring circuits with PLd/PLe performance level verification, and physical structural stress-relief validation for the frame under maximum hydraulic load tonnage.
Furthermore, structural rigidity plays a vital role in compliance and performance. Standard hydraulic bending machines subjected to heavy cycling can suffer structural fatigue or elastic frame deformation, causing angular variation along the worktable. Leading certified bending machine manufacturers utilize heavy-duty Q235B or Q345B steel plates, annealed in tempering furnaces to relieve internal stress prior to precision machining on floor-type CNC boring mills. This structural stability guarantees that safety interlocks, backgauge axes (X, R, Z1, Z2), and mechanical crowning compensation systems maintain calibration over decades of continuous 24/7 industrial duty.
Electro-Hydraulic Servo Synchronization & Y1-Y2 Independent Control
The core technological evolution of modern CE certified CNC press brakes lies in the shift from mechanical torque-tube synchronization to electro-hydraulic servo closed-loop control. In a dual-axis Y1-Y2 press brake architecture, the left and right hydraulic cylinders are controlled independently by proportional servo valves (such as Hoerbiger or Rexroth) fed with position feedback from high-resolution optical linear encoders mounted directly to the machine's C-frame side plates.
By measuring the relative displacement between the bed and ram without interference from frame deflection under tonnage, the CNC controller (e.g., Delem DA-66S/DA-69T or Cybelec CybTouch) recalculates the valve opening parameters at a cycle time of under 1 millisecond. This real-time feedback loop ensures absolute ram parallelism even during off-center bending operations, maintaining bend angle precision within ±0.3° across sheet lengths ranging from 2,000mm up to 12,000mm tandem press systems.
Strategic Sourcing Analysis
Future Procurement Trends in CNC Bending Technology
Key technological shifts, energy efficiency mandates, and automated integration paradigms shaping global procurement decisions for sheet metal fabrication plants over the next decade.
Hybrid Eco-Servo Drive Systems
Traditional hydraulic bending machines run continuous induction motors, wasting energy in idle states. Next-gen procurement prioritizes hybrid servo systems (e.g., eEVO or Servo-Variable Speed Drives) that operate hydraulic pumps only during ram motion, reducing energy consumption by up to 60-70% while lowering oil operating temperatures and extending seal lifespans.
AI-Driven Real-Time Angle Correction
Material thickness variances and tensile strength inconsistencies lead to springback errors. Strategic buyers now mandate real-time laser or contact angle measuring devices (such as Iris Plus or Lazer Safe LAMS). These sensors measure the bend angle dynamically during the stroke and instantly signal the CNC controller to adjust bottom dead center (BDC) on the fly.
Automated Robotic Bending Cells
With global skilled labor shortages expanding, automated bending cells equipped with 6-axis industrial robots (KUKA, ABB, or Fanuc) integrated with automatic tool changers (ATC) are transforming high-mix, low-volume production. Automated sheet thickness detection and automatic gripper adjustments eliminate manual setup overhead completely.
Offline 3D Programming & Digital Twins
Industry 4.0 integration allows factory managers to import STEP or IGES files directly into CAD/CAM software (such as AutoPOL, Radan, or BySoft). The software performs automatic bend sequence calculations, collision detection, and tool selection, uploading validated CNC code to the machine over local IoT networks without interrupting active production.
Mechanical CNC Dynamic Crowning
Hydraulic deflection crowning is increasingly replaced by motor-driven CNC mechanical wedge crowning tables (e.g., Wila or System Rolmeri style). These mechanical systems calculate precise wave deflection curves across the bed length, ensuring uniform bend angles from tip to tip without hydraulic heat decay or valve drift issues.
Traceable IoT Maintenance Diagnostics
Modern machine buyers expect integrated telemetry: hydraulic oil condition monitoring, pump pressure logs, stroke cycle counters, and remote cloud diagnosis. OEMs offering built-in remote service capabilities significantly reduce factory downtime and lower total cost of ownership (TCO) across the equipment lifecycle.
Industry Roadmap & Tech Evolution
Evolution of Metal Formability: From Mechanical to Smart Servo
Tracing the engineering trajectory of metal bending machinery from early mechanical friction clutch systems to ultra-precise electric and hybrid servo CNC solutions.
Historical Milestones & Technological Generation Jump
The metal fabrication landscape has undergone four distinct technological revolutions over the past five decades. Understanding these structural changes enables procurement directors to select machine specifications tailored precisely to their production volume, plate thickness requirements, and precision tolerances:
- Generation 1 (Mechanical Press Brakes): Powered by flywheel energy and mechanical friction clutches, these machines lacked stroke control, required manual shimming for deflection, and presented high operator risk due to continuous ram cycling without emergency stop capabilities.
- Generation 2 (Hydraulic Torsion Bar Machines): Introduced hydraulic cylinder actuation synchronized by a mechanical torsion rod spanning the upper beam. While safer and capable of stroke adjustment, ram tilting was limited, and off-center bending caused severe mechanical twist.
- Generation 3 (Electro-Hydraulic Servo CNC Press Brakes): Introduced independent Y1-Y2 proportional valve control guided by linear encoders. Enabled multi-axis backgauges (X, R, Z1, Z2, X-Prime), automatic hydraulic or mechanical crowning, and high-speed working modes complying with CE safety directives.
- Generation 4 (Direct-Drive All-Electric & Hybrid Servo Systems): Eliminates or drastically reduces hydraulic oil reliance using heavy-duty planetary ball screws or belt-pulley drive systems. Delivers sub-micron positioning, ultra-fast ram acceleration (up to 220mm/s), and near-silent operation with zero thermal oil expansion errors.
Technical Comparison Matrix: All-Electric press brakes excel in thin sheet metal application (0.5mm - 4.0mm) requiring high speed and low energy usage. Heavy plate bending (6.0mm up to 40mm structural steel) remains the undisputed domain of high-tonnage Electro-Hydraulic Servo Press Brakes ranging from 160 Tons to 2,000 Tons capacity.
Enterprise OEM/ODM Authority
Why Partner With Our TÜV Rheinland Audited Facility
Combining state-of-the-art metal structural fabrication, rigorous quality engineering, transparent international audit documentation, and tailored custom manufacturing solutions.
2,000 m² Audited Workshop
Our custom manufacturing facility in Guangzhou features dedicated structural welding bays, floor boring machine zones, electrical assembly clean areas, and final assembly testing bays verified on-site by TÜV Rheinland third-party inspectors.
69+ Skilled Engineers & Technicians
Our in-house R&D team integrates mechanical engineering, hydraulic circuit design, electrical PLC programming, and software customization under one roof, ensuring full alignment across hardware and control UI.
Full Customization & ODM Capability
From throat depth extensions (up to 600mm), daylight height modifications, specialized tooling designs, to custom painted cabinet branding and multi-language CNC software integration—we deliver fully bespoke machinery built to client specs.
Export Presence in 60+ Countries
Our machines are operating in metal processing centers, automotive stamping facilities, enclosure manufacturing plants, and equipment OEM workshops across Europe, North America, Latin America, the Middle East, and Southeast Asia.
Export-Ready Protective Packaging
Prior to shipment, every bending machine undergoes 72-hour continuous pressure testing. Motion axles are locked with steel transport brackets, optics and monitors are vacuum-wrapped, and frames ship in fumigation-free plywood export cases with photo loading verification.
Comprehensive Lifecycle Support
Each delivery includes complete electrical schematic diagrams, hydraulic piping manuals, operator video tutorials, spare parts kits, and lifetime remote diagnostic support provided directly by senior commissioning engineers.
Procurement Guide
Frequently Asked Buyer Questions
Detailed technical answers to the most common questions asked by global procurement teams, machinery distributors, and sheet metal factory owners.
How do I verify if a bending machine manufacturer's CE certification is genuine?
To ensure CE authenticity, request the complete EC Declaration of Conformity document along with the official Notified Body (NB) audit test report. Verify the 4-digit Notified Body number on the official NANDO database of the European Commission. Genuine compliance must reference compliance with EN 12622 for hydraulic press brakes and EN ISO 12100 for safety risk analysis, backed by physical test verification of light curtain stopping distances.
What is the standard formula for calculating bending force (tonnage requirements)?
Bending force (P in Tons) for air bending mild steel (tensile strength ~450 MPa) is estimated using the formula: P = (650 × S² × L) / V, where S is material thickness in mm, L is sheet bending length in meters, and V is die V-opening width in mm (typically V = 8 × S). For stainless steel, multiply the resulting tonnage by 1.5×; for aluminum, multiply by 0.5×. Our engineering team can provide precise tonnage calculations based on your CAD drawings.
What is the difference between Hydraulic Crowning and Mechanical CNC Crowning?
Hydraulic crowning uses auxiliary cylinders built into the lower bed to push the table upward under pressure. While effective, hydraulic oil temperature fluctuations can cause slight variations over long runs. Mechanical CNC Crowning utilizes precision slant wedges driven by a stepper/servo motor controlled by the CNC. It offers parabolic curve precision, higher accuracy across the entire length, zero thermal drift, and longer maintenance intervals.
Does UPT Machinery support full custom structural OEM/ODM modifications?
Yes. We offer extensive structural and functional customization: extended frame throat depths (400mm to 650mm), expanded daylight openings for deep box bending, custom backgauge configurations up to 6-axis (X, R, Z1, Z2, X1, X2), custom paint colors, private label branding, and installation of specialized tooling systems (Promecam, Wila, or Trumpf style).
What after-sales support and installation guidance do you provide for international shipments?
Every machine is accompanied by comprehensive electrical schematics, hydraulic flow charts, commissioning video series, and an operating manual. We provide remote online commissioning support where our engineers guide your team through electrical hookup, zero-point calibration, and program setup. Replacement spare parts (relays, valves, seal kits) are stocked and dispatched via expedited air freight when required.
How does UPT Machinery protect heavy machines against corrosion and freight damage during sea transport?
All bright metal machined surfaces (die beds, ram guides, backgauge rails) are treated with heavy-duty anti-rust oil film and sealed with moisture-absorbent barrier foil. Hydraulic cylinders are retracted, and the ram is resting on solid wooden support blocks with mechanical lock pins engaged. Equipment is anchored inside open-top or flat-rack containers using heavy-duty steel wire ropes and turnbuckles.
Direct Sourcing & Quotation
Request Equipment Specification & Factory Price List
Send your metal sheet material specs, thickness range, bending length requirements, or CAD part drawings. Our senior technical team will return a complete machine specification matrix, tooling recommendation, and factory direct quotation within 24 hours.